Precision manufacturing environments, semiconductor fabrication cleanrooms (ISO Class 1 to 5), pharmaceutical validation laboratories, and aggressive chemical fume exhaust systems demand an uncompromising standard of air purity. In these critical contamination-sensitive settings, traditional loose-fill granular carbon trays, trays with felt backing, or low-grade fibrous adsorption pads introduce an unacceptable operational risk: carbon dusting, media shedding, and micro-particulate migration. In microelectronics or sterile pharmaceutical processing, even microscopic carbon fines can cause irreversible wafer defects, optical contamination, or batch rejection.
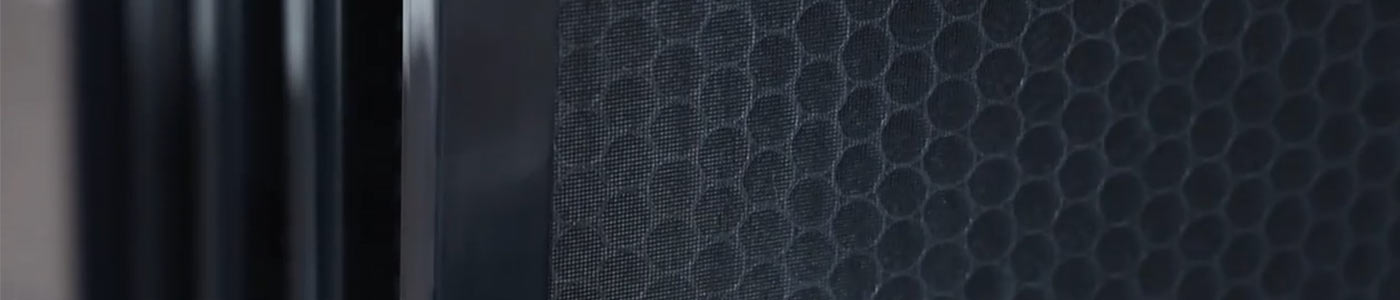
Extruded honeycomb chemical filters are engineered specifically to eliminate these vulnerabilities. By merging high-density molecular adsorption with monolithic structural integrity, these modules provide rigorous laminar airflow channels and robust volatile organic compound (VOC) removal without particle shedding.
The Engineering Mechanics of Monolithic Extruded Honeycomb Structures
Unlike traditional granular beds prone to settling, fluid channeling, or mechanical breakdown under high vibration, honeycomb chemical modules are manufactured by extruding activated carbon, high-purity binders, and specialized catalytic additives into a rigid, monolithic honeycomb matrix featuring thousands of parallel micro-channels.
Uniform Laminar Flow Dynamics: The precise geometric cell structure guides incoming air through straight, unobstructed parallel pathways. This prevents turbulent eddy formation, eliminates localized dead zones, and maintains an exceptionally uniform velocity profile across the entire filter face.
Zero Carbon Dusting and Zero Media Migration: Because the active carbon is structurally bonded within a solid extruded matrix rather than held loose in trays or panels, these filters eliminate carbon fine migration entirely. This makes them the definitive industry standard for cleanrooms where particulate counts must remain strictly controlled.
Optimized Pressure Drop vs. Adsorption Capacity: Honeycomb designs achieve a balanced initial pressure drop (90 Pa to 130 Pa at rated airflow) while packing 8 kg to 15 kg of active carbon mass into structured channels engineered for an optimal molecular dwell time of 0.1 s to 0.15 s.
Critical Cleanroom and Exhaust Applications for Molecular Control
Different high-purity industrial sectors rely on honeycomb chemical filtration units to target specific molecular contaminants:
Semiconductor and Microelectronics Fabrication: Neutralizes airborne molecular contamination (AMC), including acids (HCl, HF), bases (NH3), and condensable organic outgassing that cause micro-corrosion and haze defects on silicon wafers during photolithography and wet-etching.
Laboratory Fume Hood Exhaust Streams: Captures aggressive solvent vapors, halogenated hydrocarbons, and hazardous chemical reagents safely before air is scrubbed or discharged into atmospheric compliance streams.
Hospital Isolation Wards and Pharmaceutical Cleanrooms: Removes hazardous pharmaceutical vapors, sterilizing agents (such as hydrogen peroxide vapor residues), and persistent chemical odors from sensitive critical-care return air loops.
Side-by-Side Technical Specification Matrix
| Performance Parameter | Extruded Honeycomb Chemical Modules | Traditional Granular Carbon Trays |
| Structural Matrix Type | Monolithic extruded parallel micro-channels | Loose-fill granular carbon in metal trays |
| Active Carbon Mass per Unit | 8 kg – 15 kg (Structured block) | 10 kg – 20 kg (Loose fill) |
| Initial Pressure Drop (@ Rated Flow) | 90 Pa – 130 Pa (Stable laminar flow) | 140 Pa – 220 Pa (Prone to channeling) |
| Carbon Dusting / Shedding Risk | Zero (Solid bound matrix) | High (Fines migration over time) |
| Face Velocity Target | 0.4 m/s – 0.8 m/s | 0.3 m/s – 0.5 m/s |
| Primary Cleanroom Suitability | ISO Class 1 – 5 Critical Cleanrooms | General industrial odor control |
Securing High-Purity Cleanroom Filtration Solutions
As an established B2B source manufacturer with over 20 years of production expertise, we engineer high-purity chemical filtration units built to strict international cleanroom standards:
For cleanrooms, laboratories, and zero-dust exhaust setups: [Explore Honeycomb Chemical Air Purification Units]
For heavy-duty industrial high-airflow installations, reference our primary framework: [How Do Industrial Activated Carbon Filters and V-Bank Systems Maximize VOC Removal?].
Need custom dimensions, specialized frame configurations, or factory-direct wholesale quotations? [Request a Free Technical Datasheet and Factory Quotation Today] to consult directly with our senior application engineers.